Introduction
SAP S/4HANA for Manufacturing promises real-time visibility and tighter production cycles, but the common assumption about why these migrations fail or stall is wrong: it’s rarely the technology. Manufacturing landscapes form dense webs of interdependent processes. Production planning, procurement, quality checks, and warehouse movements all trigger one another. Migration timelines often fail not because of missing modules, but because organizations underestimate how tightly these processes connect before they sequence the cutover.
Get the sequencing and governance right, and S/4HANA for Manufacturing delivers exactly what it promises: real-time production visibility, tighter planning cycles, and a single digital backbone instead of departmental silos. Get it wrong, and the same interdependency that makes S/4HANA powerful is what turns one delayed module into a cascading production risk.
This guide covers the modules that actually drive the transformation; the migration approach decisions (Greenfield vs. Brownfield vs. Hybrid) that determine your risk profile; and the risks most migration guides leave out entirely: process misalignment, integration gaps, and what happens after go-live if governance lapses.
What Is SAP S/4HANA for Manufacturing?
SAP S/4HANA Manufacturing is an intelligent ERP solution which is aimed at supporting the end-to-end production chain. It is a platform that integrates planning, execution, logistics, and analytics.
In contrast to the classical ERP systems, it is based on an in-memory database, which allows real-time processing of the data. This implies that manufacturers are able to respond more rapidly to demand variations, supply issues, and operational problems.
The essence of SAP S/4HANA is connectivity between different manufacturing processes to one digital backbone. Other departmental common data can also be accessed by team members as opposed to working in silos.
The main modules that enable the manufacturing transformation.
Before planning any migration, it's important to understand the core modules that power SAP S/4HANA for Manufacturing:
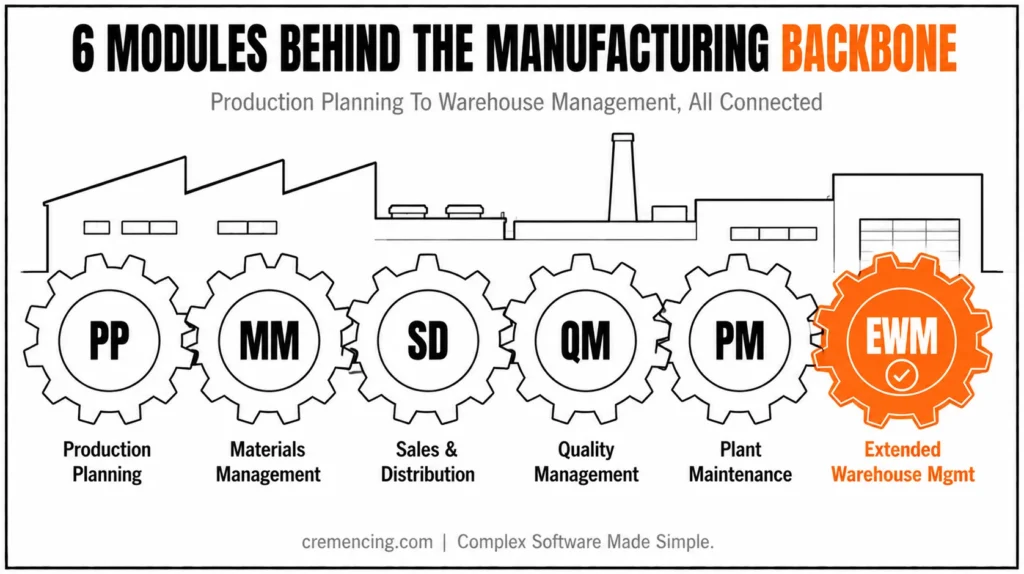
- Production Planning (PP): Processes the production orders, scheduling, and capacity planning.
- Materials Management (MM): This is involved in procurement, inventory, and supplier coordination.
- Sales and Distribution (SD): Refers to the planning of demand for production.
- Quality Management (QM): Ensures the quality of the products during the production process.
- Plant Maintenance (PM): Helps in the maintenance of equipment and reduces downtime.
- Extended Warehouse Management (EWM): This is an optimization of operations and logistics in the warehouse.
Two additional capabilities matter for most modern manufacturing landscapes:
- Production Planning and Detailed Scheduling (PP/DS): replaces classic MRP for manufacturers with complex constraints (finite capacity, sequence-dependent setup times); increasingly the default planning engine in S/4HANA rather than an add-on.
- Digital Manufacturing (SAP DM): shop-floor execution and machine-level integration, connecting MES-level data back into S/4HANA for real-time production tracking; this is where the “real-time visibility” benefit actually gets its data from, rather than from the ERP layer alone.
All modules are very important. Their collaborative efforts create a networked manufacturing ecosystem.
The SAP S/4HANA for Manufacturing Migration Process
Step 1: Explore Your Present Landscape.
You should clearly understand your existing systems before making a decision on whether or not to migrate to SAP S/4HANA.
This includes determining any legacy processes and custom development and integration points. This is something that not all manufacturers are taking lightly, and this can bring about other problems.
Such a thorough analysis can guide you to know what to retain, what to enhance, and what to eliminate.
Step 2: Outline Your Migration Strategy.
There are different migration approaches:
- Greenfield (new implementation): A clean start with lean processes.
- Brownfield (system conversion): Renovation of current systems.
- Hybrid strategy: A combination of the two strategies.
For manufacturing specifically, the choice carries more weight than in other industries: Brownfield conversion preserves existing PP/QM configuration and historical production data but also carries forward any accumulated custom code and undocumented process workarounds—exactly the kind of technical debt that later shows up as testing delays.
Greenfield gives a clean re-implementation against SAP best-practice manufacturing processes but requires revalidating every custom quality check, production order type, and interface from scratch. Weigh your business goals, system complexity, and timeline to make the right decision.
Greenfield vs. Brownfield vs. Hybrid for Manufacturing
| Approach | Best fit when | Manufacturing-specific risk |
|---|---|---|
| Greenfield | Heavily customized legacy system, appetite for process redesign | Full re-validation of production orders, QM inspection plans, PP variant configuration |
| Brownfield | Stable, well-governed current landscape | Carries forward custom code and technical debt into the new system |
| Hybrid | Selective modernization of high-impact modules only | Requires strong integration governance between converted and re-implemented areas |
Step 3: Plan out significant modules.
Migration of all modules cannot be done simultaneously.
To start with, focus on high-impact areas, i.e., production planning and inventory management. This lessens the risk and guarantees the continuation of business. A gradual process enables teams to change at a slow pace, and operations are not disturbed.
Step 4: Migration and Preparation of Data.
The data of any SAP project is one of the largest issues in any SAP project.
Mistaken or redundant information may lead to severe problems once it has been migrated. Cleaning and validating data, as well as its transfer to SAP S/4HANA, is crucial.
This step can take much more time than one would expect, but not doing so will cause problems in the long term. Poor data quality is another typical error.
Step 5: Testing and validation.
It will be tested to make sure that all processes are operating effectively in the new system.
This involves functional testing, integration testing, and user acceptance testing. The manufacturing processes must be checked with caution in order not to cause any disruption in the production process.
Step 6: Go-Live and optimization.
Go-live stage is critical. Minor problems have the potential to affect production.
After the deployment, it requires continual monitoring and optimizing. This will ensure that the system is able to provide desired performance and value.
SAP S/4HANA for Manufacturing Benefits & ROI.
Organizations that successfully implement SAP S/4HANA often achieve measurable improvements in their operations.
Key Benefits
- Real-Time Visibility: See real-time production and inventory data.
- Enhanced Productivity: Minimize human activities and mistakes.
- Better Planning Accuracy: Co-ordinate demand and production.
- Less Downtime: Predictive maintenance enhances the reliability of equipment.
Quantifiable Outcomes
| Area | Improvement |
| Production efficiency | 15–25% increase |
| Inventory reduction | 10–20% |
| Order processing time | 30–50% faster |
| Maintenance costs | 10–15% reduction |
These improvements have a direct impact on profitability and operational activities.
Along with numbers, SAP S/4HANA assists in making superior decisions. The managers will be capable of responding to changes within a few seconds and maximize production in real time.
Errors to avoid in the process of Migration
When SAP S/4HANA for Manufacturing projects fail to deliver expected results, technology often isn’t the problem. Preventable mistakes usually are.
One of the main problems is underestimation of the complexity of the systems. The processes in manufacturing are interdependent, and any slight change can have far-reaching effects.
Poor data quality is another typical error. When the wrong data is transferred, it leads to operating difficulties and delays.
The lack of user training is also among the challenges that companies might have to encounter. To be able to carry out its functions, even a perfect system cannot do its tasks without the knowledge of the users using the system to its full potential.
Over-customization is another risk. The process of trying to replicate the old processes instead of the best practices in SAP S/4HANA reduces the value of SAP S/4HANA.
Finally, the absence of effective project governance brings about a scenario of perplexity and failure to meet deadlines. There must be clear ownership as well as accountability.
Secret Migration Dangers: The Majority of Companies are Blind.
The majority of guides cover technical challenges yet fail to mention other, more serious perils.
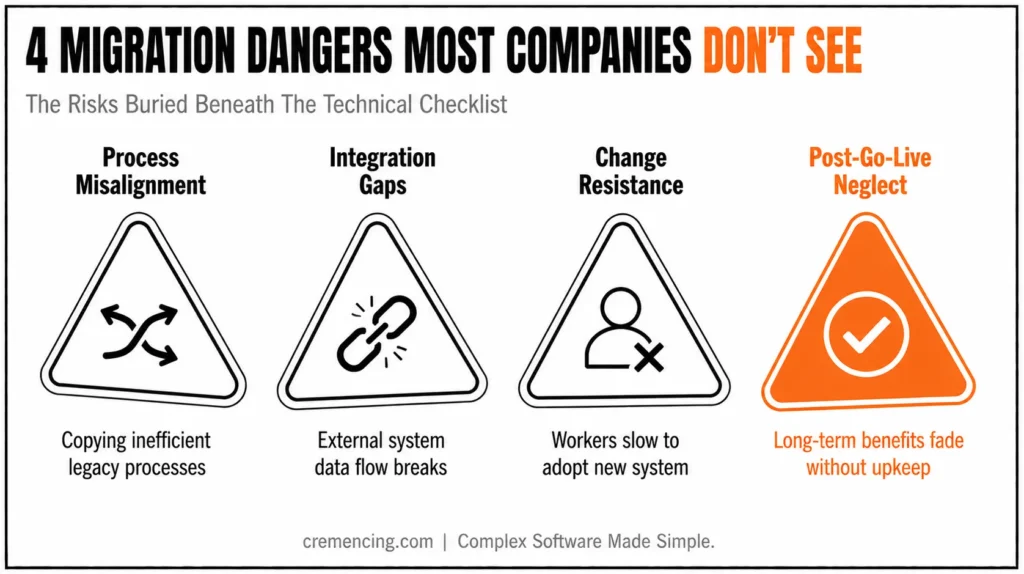
Teams often overlook process misalignment during SAP S/4HANA for Manufacturing projects.
When companies transfer an inefficient legacy process without improving it, they miss a major opportunity to increase efficiency. Integration gaps create another hidden risk, especially when connected systems, data flows, and dependencies remain unclear.
The systems employed in manufacturing are usually connected with external systems. Without making appropriate integrations, there might be a break in data flows.
The main challenge is also change resistance. Workers may also be opposed to the new systems, which slows down the process and makes it less effective.
Finally, long-term effectiveness of post-go-live carelessness can decrease the long-term effects. Achieving the full benefits of SAP S/4HANA will require continuous improvement.
Considering a relocation of your SAP S/4HANA manufacturing?
The preliminary step is to discover what your high-risk areas are and prioritize the key modules so that you will never make costly errors before it happens.
Conclusion
The modules, the migration approach, and the risk list in this guide all point to the same underlying truth: S/4HANA for Manufacturing doesn’t fail on technology; it fails on sequencing and governance. The organizations that treat module rollout as a deliberate, risk-ranked sequence, not a single big-bang cutover, are the ones that convert the platform’s real-time visibility into an actual production advantage rather than a longer list of interdependent systems to keep synchronized.
If you’re at the stage of choosing Greenfield, Brownfield, or Hybrid, that decision is the highest-leverage one in this whole guide get it wrong and every subsequent step inherits the risk.
FAQ:
1. What is different about SAP S/4HANA as compared to traditional ERP systems?
It provides real-time processing of data and built-in analytics, which can be used to make decisions faster.
2. What is the crucial module of manufacturing?
Production Planning (PP) is necessary, but it is preferable to do it along with other modules.
3. Migration: How many days was the duration of migration?
It is complex in nature, and most projects take 6-18 months.
4. What is the largest risk of migration?
The most prevalent risks are the low quality of the data and the absence of planning.
5. Will small manufacturers get a competitive advantage with SAP S/4HANA?
Yes especially when there are scalable deployment programs, which are developed according to the size of the business.
6. Does S/4HANA Manufacturing support process manufacturing (PP-PI) as well as discrete manufacturing?
Yes S/4HANA supports both discrete (PP) and process manufacturing (PP-PI) with process orders, recipe management, and batch handling, though the module emphasis and configuration differ by industry.
7. What’s the difference between embedded EWM and decentralized EWM?
Embedded EWM runs inside the S/4HANA system itself (typical for on-premises); decentralized EWM runs as a separate system connected via integration, which is the required model for S/4HANA Cloud and for landscapes with very high warehouse transaction volumes.
8. Can manufacturers migrate module-by-module instead of all at once?
Partial migration is possible but requires careful interface design between converted and legacy modules during the transition. This is essentially what the “hybrid strategy” approach formalizes, rather than an ad hoc partial cutover.